Manufacturing testing covers traction- and storage-battery lines, vehicle final assembly and end-of-line stations, and incoming and in-process inspection of core components — organised around how cycle time, consistency and a common data basis can hold at once on one modular architecture.
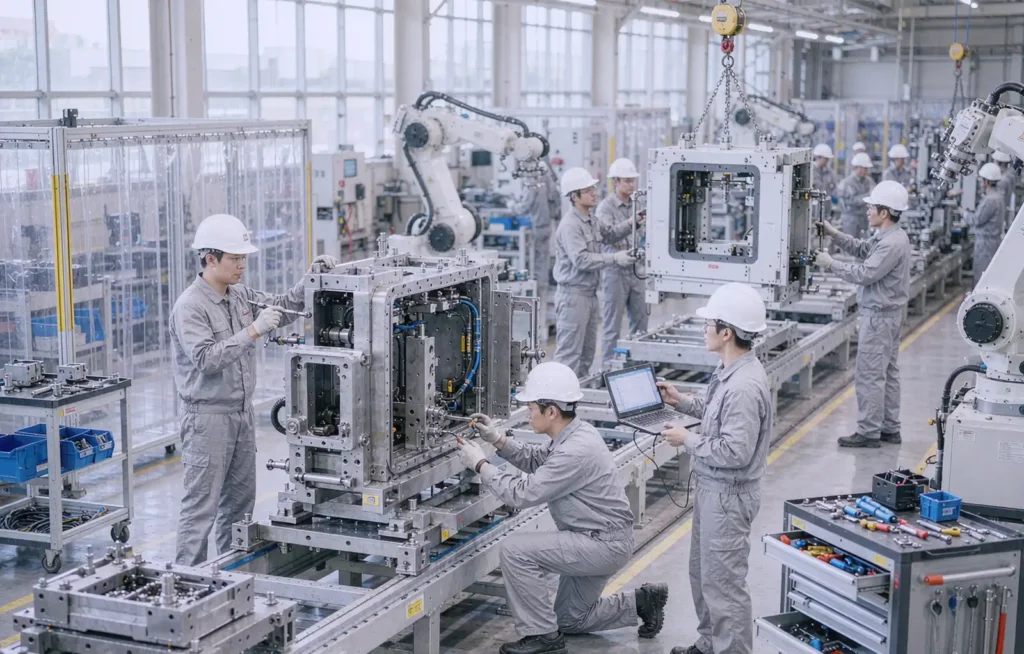
On a production line, the test section governs cycle time, yield and line-stop risk at once
Adding test items consumes cycle time; compressing cycle time reduces coverage. Where stations run serially with a fixed test-item set per station, the two can only be traded against each other. Actual cycle time during capacity ramp-up commonly deviates from the design value, and the test section is the first bottleneck to surface.
Where the same product is delivered by different integrators at different sites, test-item definitions, adjudication thresholds, data fields and report formats all differ. Quality data cannot be compared across sites, process issues must be re-analysed base by base, and experience does not transfer directly when a new base starts production.
Without a common definition of station, batch, operating condition, parameter, result and fault label, test data remains on the equipment or in dispersed reports. Anomaly clustering, root-cause analysis and threshold optimisation lack a usable data basis, and traceability requests require manual reconstruction across systems.
Cell formation and grading and battery charge/discharge testing are high-consumption operations run in parallel across many stations. With a resistive dissipation design, discharge energy leaves the process as heat and adds to the cooling load. Energy efficiency and dispatch method bear directly on operating expenditure and on transformer capacity requirements.
When an existing line takes on a new vehicle or battery model, the retrofit is normally limited to fixtures, software configuration and the addition or removal of stations, but it must be completed inside the planned line-stop window. Where the hardware platform does not support expansion at module level, the retrofit becomes an equipment replacement.
Manufacturing testing covers traction-battery and storage-battery lines, vehicle final-assembly and end-of-line stations, and incoming and in-process inspection of core components. Tsing Standard has taken part in the delivery of 149 vehicle and component lines and 49 traction-battery production bases covering 167 GWh of cell capacity, working with 36 line integrators and serving 16 battery manufacturers. The Non-Standard Business Unit currently holds 332 projects, 280 vehicle-related and 52 battery-related.
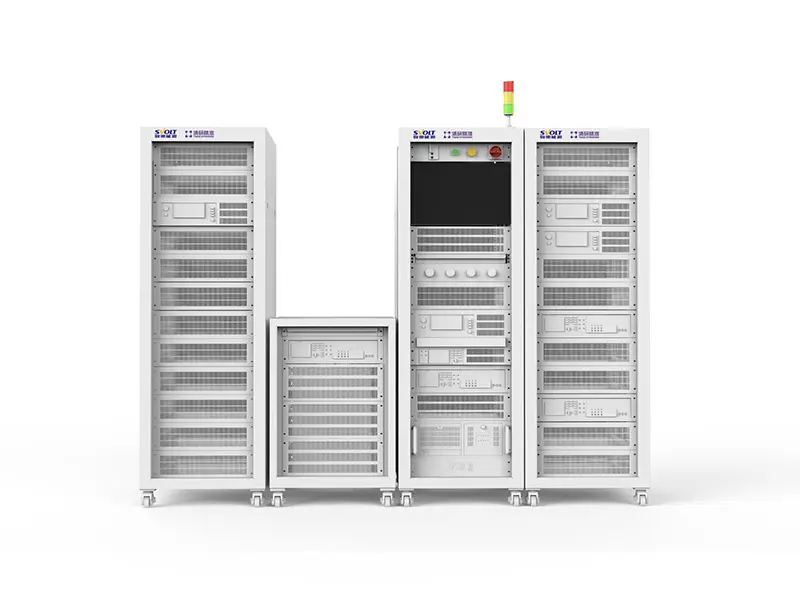
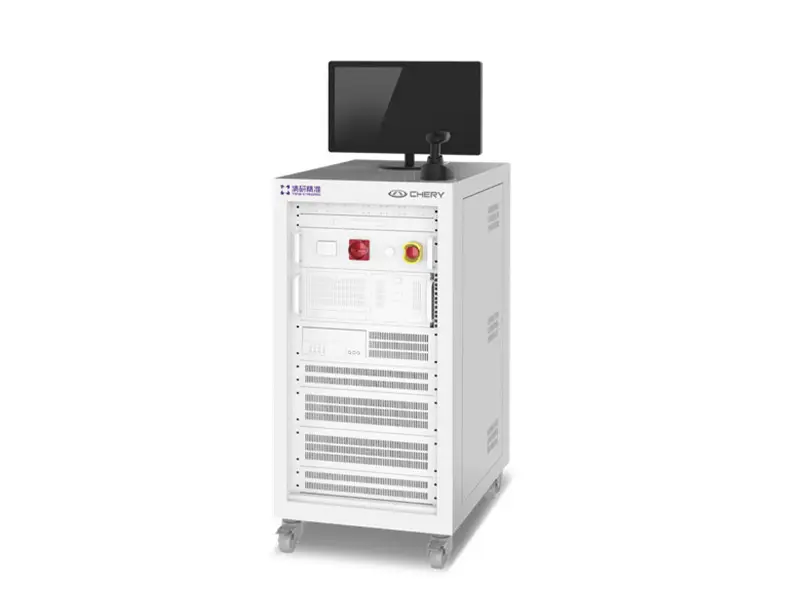
Test equipment uses a plug-in rack architecture in which cards are hot-swappable and modules are added or removed according to the test-item set. The controller card supports up to 254 units in cascade; the measurement module covers voltages to 1,000 V; the insulation and withstand module tests to 3,500 V and expands to 5,334 channels; the equipotential module supports up to 508 channels; the internal-resistance module supports up to 508 measurement channels. An electronic design reduces the number of internal connection points and the harness count, and limits the influence of temperature and humidity on measurement accuracy.
Software runs on an in-house no-code test operating system with a client-server architecture, graphical configuration and plug-in development, supporting secondary development and mainstream communication protocols, MES integration and test-data upload. Test items, adjudication thresholds and report formats are defined by configuration, so one hardware platform serves different vehicle and battery models and the scope of a retrofit converges on fixtures and software configuration.
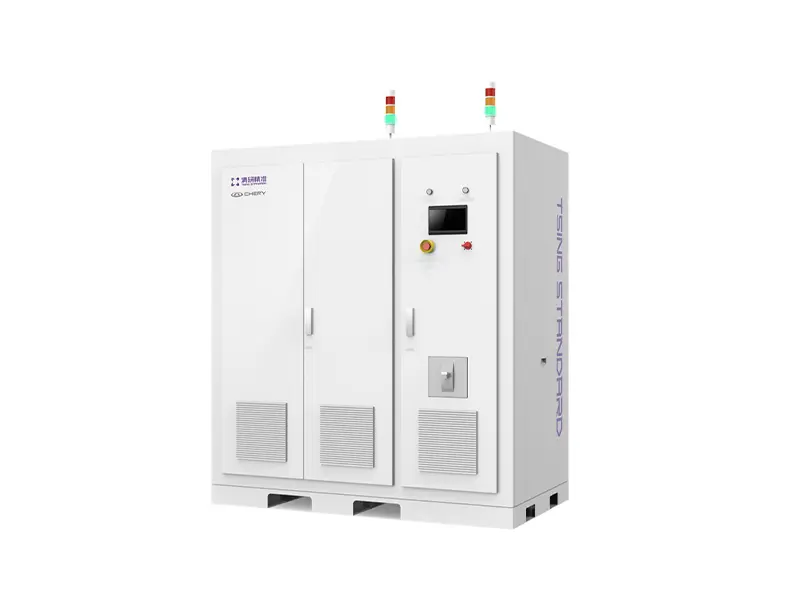
Module line, PACK line, energy storage battery line; MES docking and data uploading
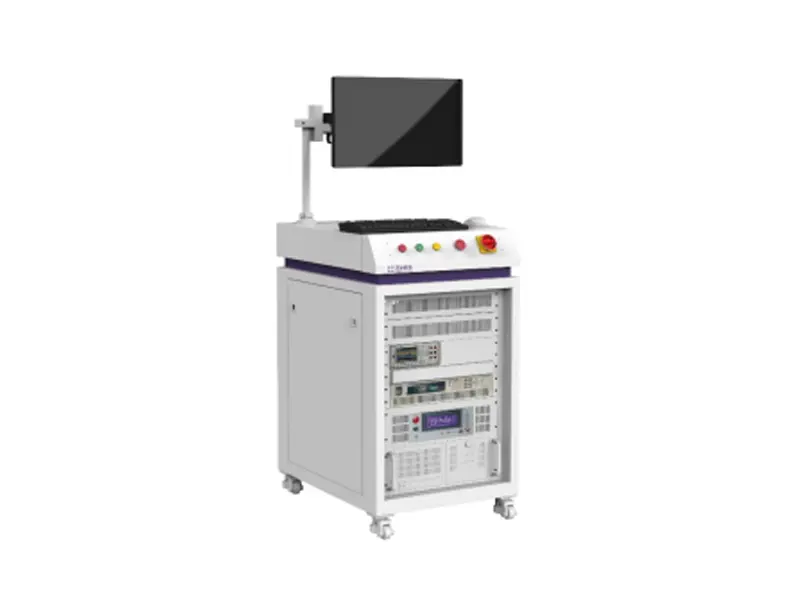
Offline basic function and insulation withstand voltage safety performance testing; 254 card cascade
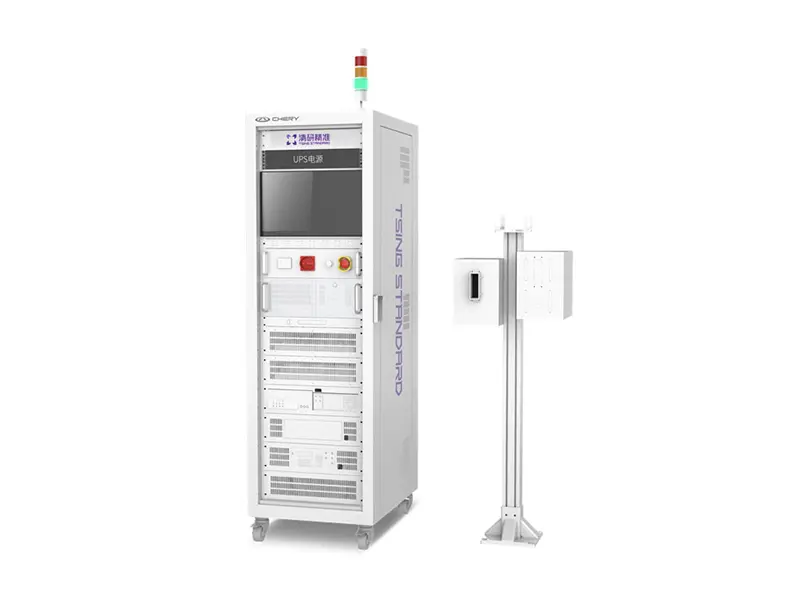
Internal consumption of feedback energy on the DC side, peak valley scheduling, and demand control; EMS Strategy and Scheduling Logic
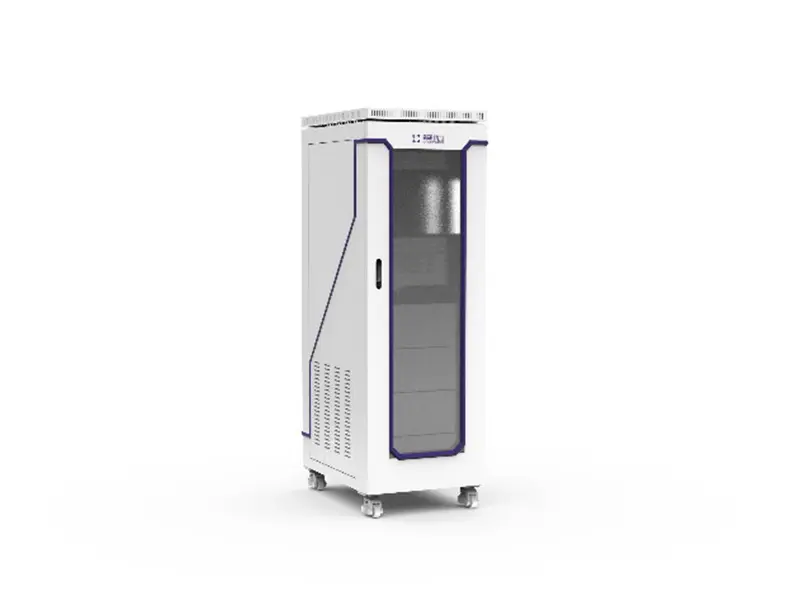
Power battery system, motor PDU、BDU、OBC、DCDC; Electrical safety, continuity, communication, high voltage sampling, signal simulation
Pressure drop method, differential pressure method, mass flow method; The standard configuration for production line level is 0-20 kPa or 0-500 kPa, which can be freely set. 0-2000 kPa is a high-pressure/customized configuration; Accuracy 0.05% F.S
Common DC bus energy efficiency feedback; The optimal feedback efficiency is ≥ 95%; Supports up to 1200 V
Plug-in cards are hot-swappable, so introducing a new vehicle or battery model limits the retrofit to fixtures, software configuration and the addition or removal of stations. The hardware platform is carried over, and the delivery cycle is constrained by the line-stop window rather than by manufacturing lead time.
A graphical test software platform developed wholly in-house, in which test items, adjudication thresholds and report formats are defined by configuration. It supports plug-in extension, mainstream communication protocols and MES integration, allowing test engineers to deploy and change line test programs without writing code.
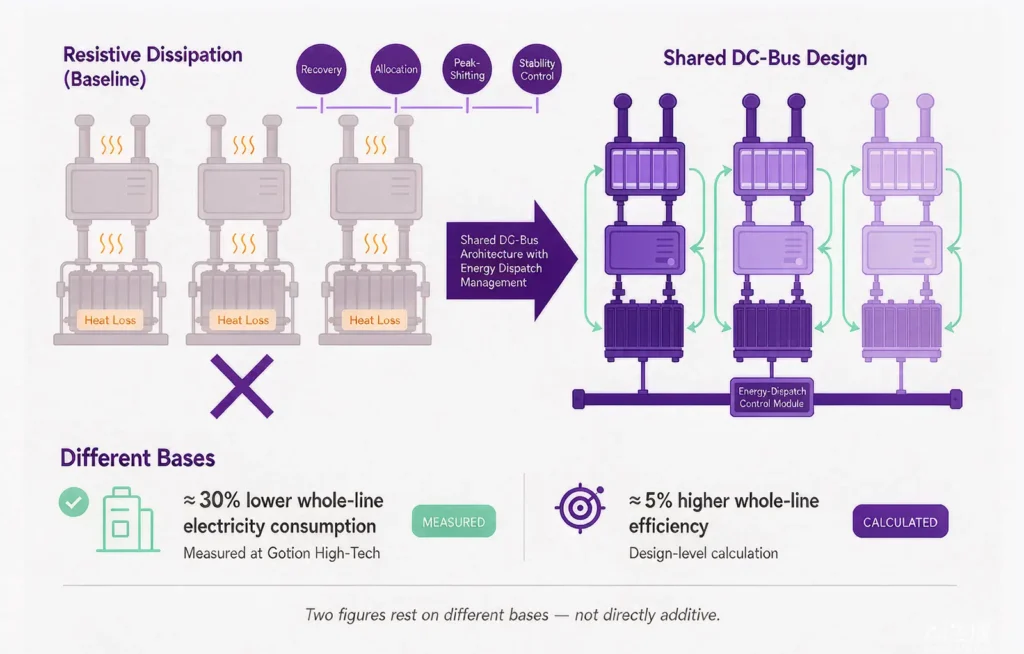
A shared DC-bus architecture reuses discharge energy internally on the DC side, with energy dispatch management providing recovery, allocation and peak-shifting. Measured at Gotion High-Tech, whole-line consumption fell by approximately 30%; the figure of approximately 5% higher whole-line efficiency is a design-level calculation. At the Liuzhou base, 99.5% of regenerated formation energy was measured as absorbed by storage.
Station, batch, parameter, result and fault label share a single data definition, making the test record auditable end to end and comparable across sites. Multi-site replication deploys the same data model, so a new base does not need to redefine test items or adjudication thresholds.
Coverage spans leak testing, safety compliance (self-insulation ≥20 GΩ, withstand to 3,500 V, 508 equipotential channels, leakage current), electrical performance, communication protocols, end-of-line inspection, traceability, fixtures and acceptance documentation, combinable into a complete test section according to the customer's process.
From a single pilot line to multi-site replication
The customer was building traction-battery and storage-battery lines simultaneously at several domestic bases and in North America, Thailand and Indonesia. The test section had to satisfy energy, cycle-time and cross-site consistency requirements at once, and new bases had to be able to reuse a proven configuration.
Delivered battery-line test systems at bases including Liuzhou and Chuzhou; end-of-line and electrical-performance retrofits at Tongcheng; the battery test system at the North America base; the Chicago Line A platform upgrade and Line B build; and installation and commissioning of Phase-2 electrical test cabinets. Scope comprised the cell test system, the energy dispatch management system and line-level system design and integration, with a three-year system-level warranty.
With a shared DC bus and energy dispatch, whole-line electricity consumption is approximately 30% lower than a resistive dissipation design, on a measured site basis. Test basis and data model are unified across bases, producing a replicable deployment baseline, and the system carries a three-year system-level warranty.
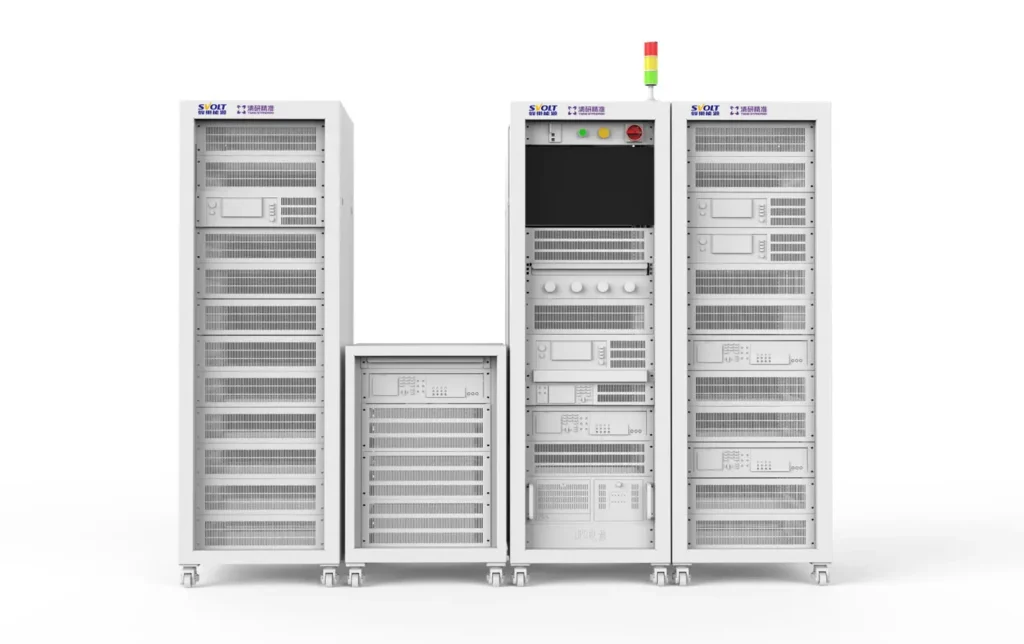
Core components on a vehicle line require incoming and in-process inspection before assembly, covering open-circuit voltage comparison, capacity, AC internal resistance, leak, multi-channel resistance signal simulation and several communication tests, all within the line cycle time.
A modular core-component test system was deployed on a wide-voltage platform, supporting parallel multi-channel resistance signal simulation, custom negative-pressure development, wide-range high-accuracy leak measurement, AC internal-resistance testing and multiple communication tests.
Test items are configured per station on a single platform, all inspection items complete within the line cycle time, and test data is uploaded on a common basis.